Chemical Industry AI-Powered Computer Vision for Safety & Hazard Prevention

Future proof chemical plants, processing facilities, and storage operations with advanced computer vision for worker protection, regulatory compliance, and operational safety excellence.
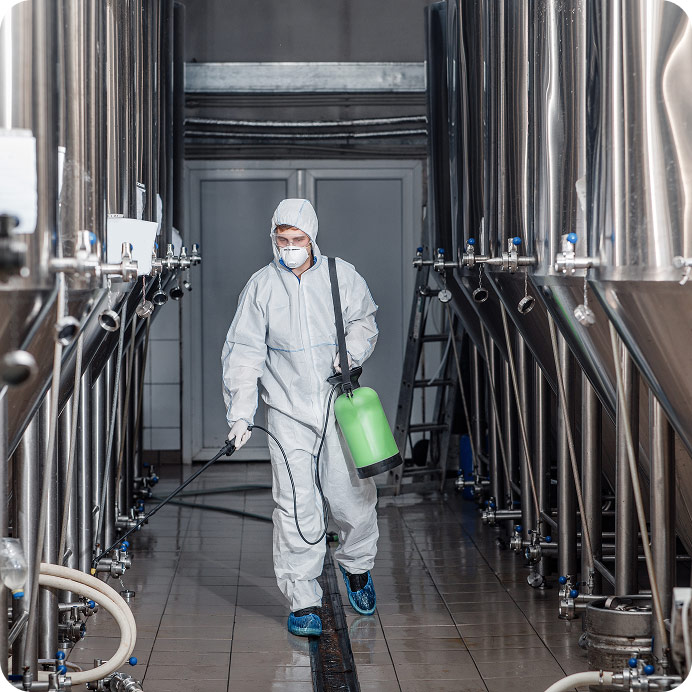
Hero Image

Advanced Chemical Safety Monitoring with AI Intelligence

Our AI-powered monitoring system continuously detects critical safety violations and hazardous conditions in toxic, corrosive, and flammable chemical environments that could lead to serious injuries, fires, explosions, or regulatory violations.
01. Prevent Before Catastrophe

Critical Chemical Safety Detection:

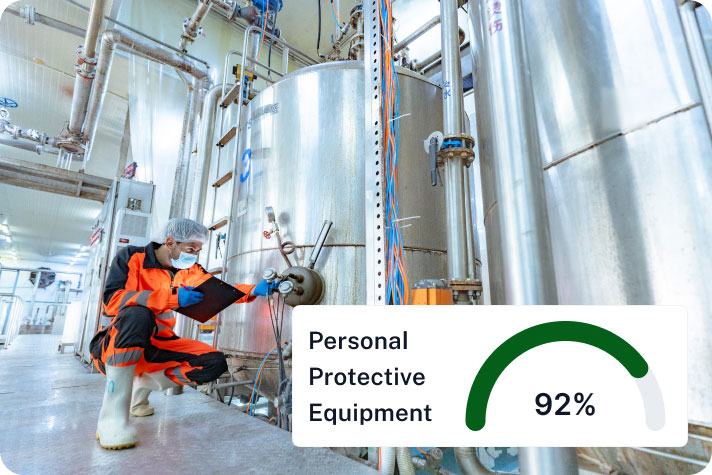
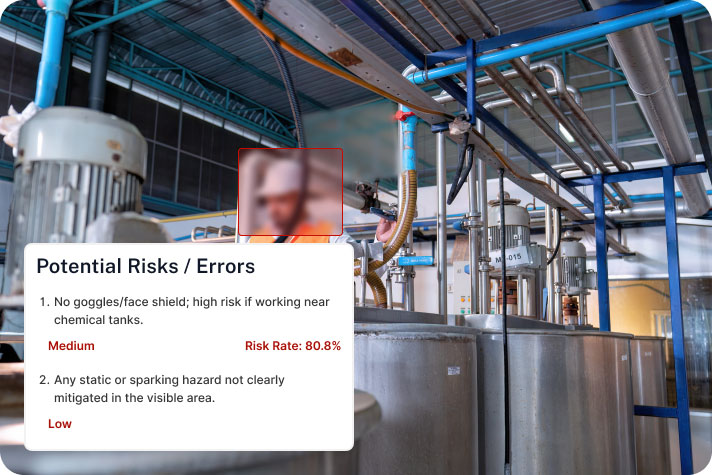
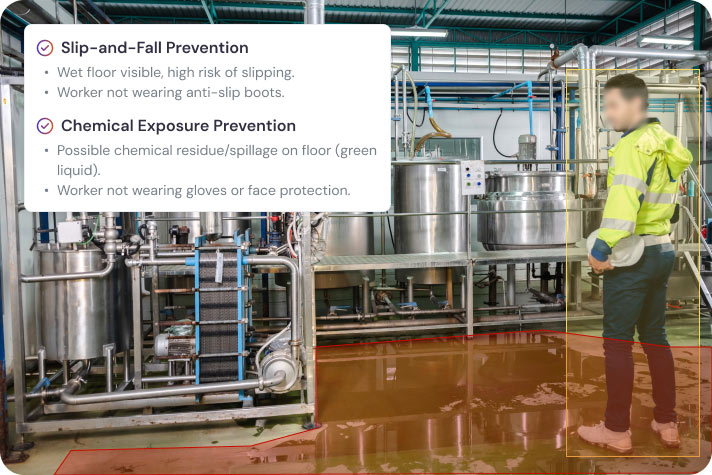
  • PPE Compliance Monitoring – Monitoring of slippery surfaces & wet floors that are common in food processing environments, with instant alerts.
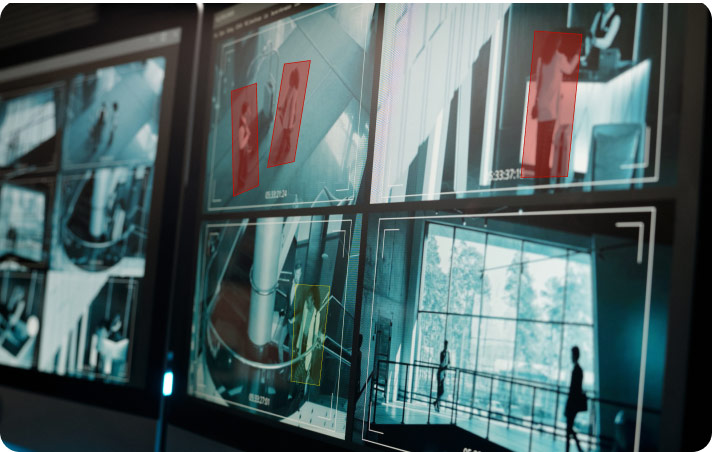
  • Vehicle Near Misses – Instantly alerts when tankers, forklifts, or equipment come dangerously close to personnel in processing zones
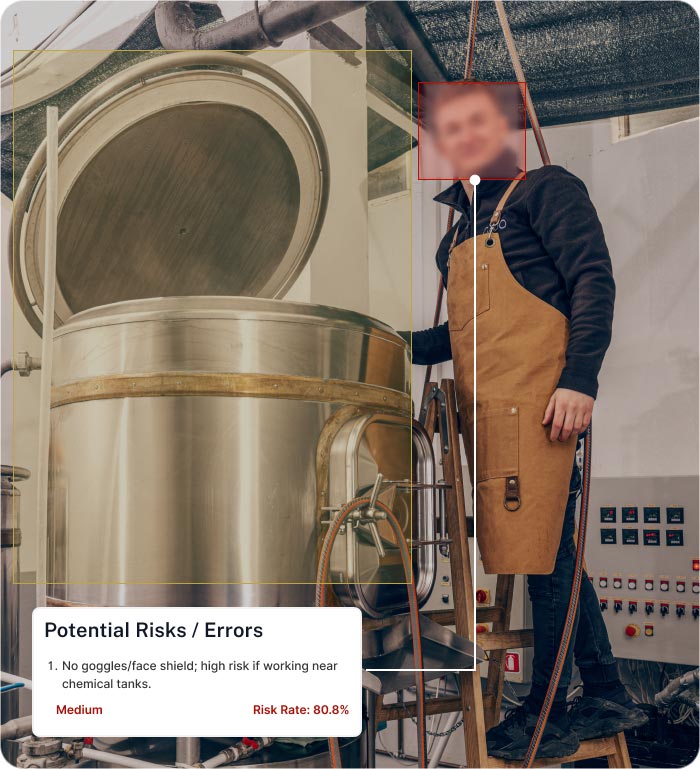
  • Confined Space Violations – Monitors unauthorized entry into tanks, vessels, & restricted chemical storage areas.
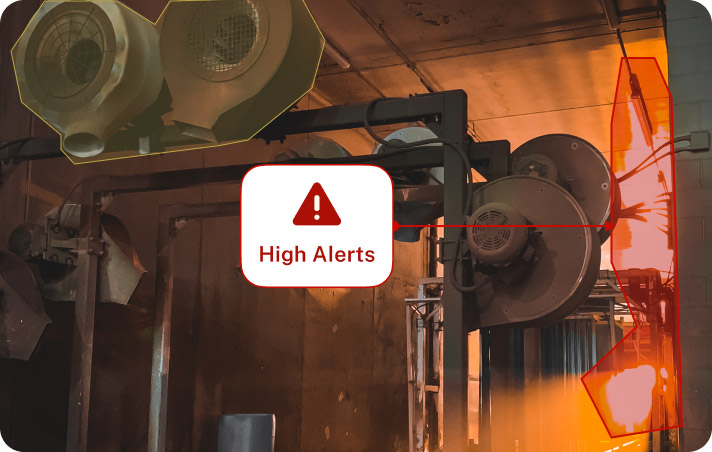
  • Fire & Explosion Risks – Detects ignition sources, overheating equipment, & unsafe conditions around flammable chemicals.
  • Chemical Exposure Prevention – Identifies leaks, spills, and vapor releases that could expose workers to toxic or corrosive substances.
  • Transfer Zone Safety – Monitors chemical loading, unloading, and transfer operations for safety protocol compliance.
  • Falls from Heights – Detects unsafe climbing, ladder misuse, or missing fall protection around elevated chemical equipment.
02. Chemical Area & Compliance Monitoring

Access Control & Hazard Zone Restrictions:

  • No entry into restricted chemical areas – Monitors sensitive processing zones, tank farms, and high-hazard chemical storage areas.
  • Confined space control – Enforces proper entry procedures for tanks, vessels, and enclosed chemical processing equipment.
  • Motion detection & heat detection – Complete coverage for restricted chemical processing areas & emergency shutdown zones
  • No smoking in chemical facilities – Detects violations in flammable chemical zones and processing areas.
  • No grouping/idling near hazards – Identifies unsafe clustering around chemical transfer zones and processing equipment.
  • Chemical handling violations – Tracks improper handling of toxic, corrosive, and flammable substances.
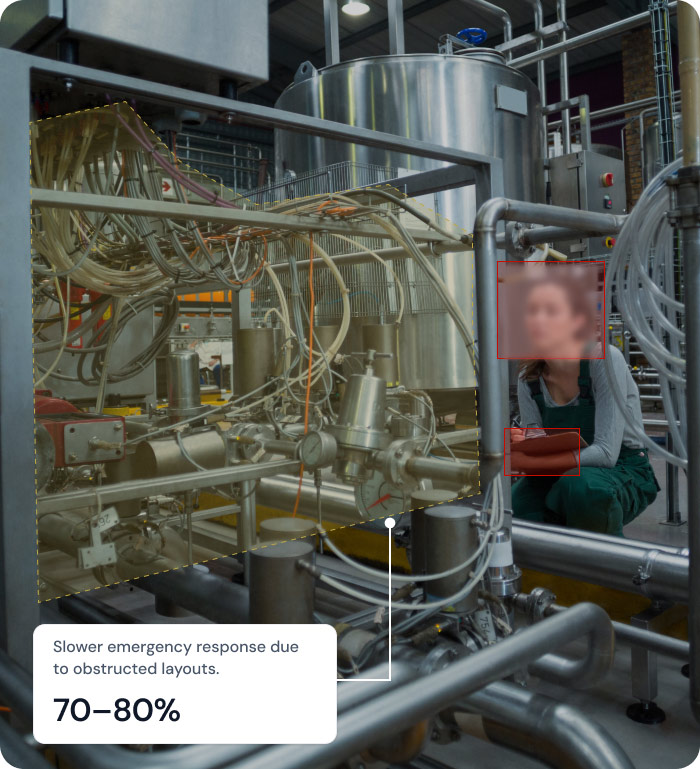
  • Housekeeping in chemical areas – Detects blocked emergency exits, spill containment issues, and poor facility maintenance impacting chemical safety.
03. Real-Time Chemical Safety Alerts

Chemical-Specific Alert Capabilities:

  • Real-time alerts – for all detected chemical safety violations and hazardous conditions.
  • Instant notifications – for chemical leaks, temperature fluctuations in processing zones, or equipment failures
  • AI-enabled analytics – prioritizing alerts by chemical hazard severity and SIF (Serious Injury and Fatality) risk level.
  • Automated incident logging – with video evidence, timestamps, and OSHA-aligned documentation.
  • Seamless integration – with existing chemical plant safety management systems and emergency response protocols.
04. Chemical Industry Analytics and Reporting

Key Performance Indicators for Chemical Operations:

  • SIF Prevention Metrics – Track serious injury and fatality prevention across chemical processing areas.
  • PPE Compliance Rates – Monitor face shield, respirator, and chemical-resistant glove usage across all shifts.
  • Chemical Exposure Incidents – Reduce toxic, corrosive, and flammable chemical exposure events.
  • Regulatory Compliance Scores – Maintain digital audit trails for chemical facility inspections and certifications.
  • Fire & Explosion Prevention – Track ignition risk mitigation and flammable chemical handling compliance.

Integration with Chemical Plant Operations

Supporting Your Chemical Processing Systems:

Our AI vision system integrates with your chemical plant management systems and safety workflows, enhancing protection across:
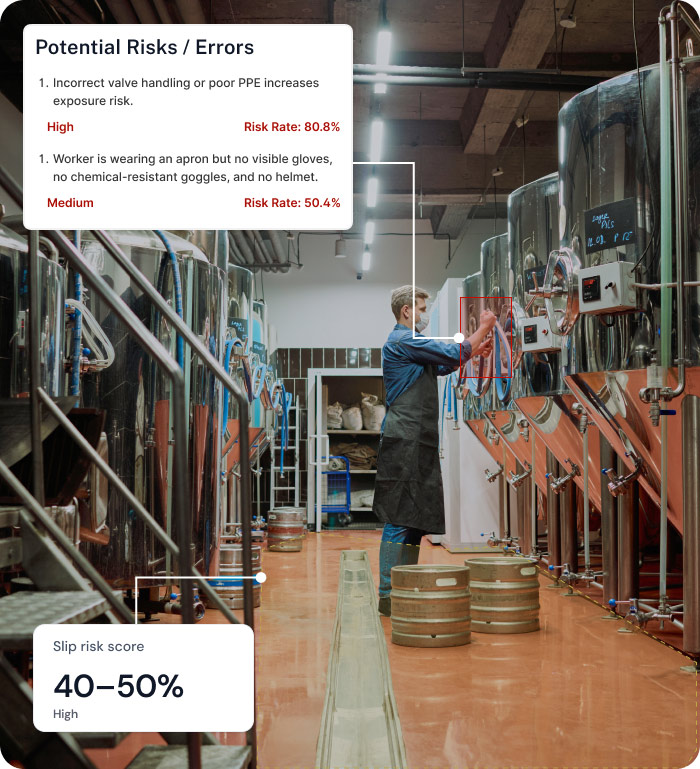
  • Tank farm monitoring and transfer operations.
  • Chemical mixing and reaction vessel safety.
  • Distillation and separation process monitoring.
  • Chemical loading and unloading dock safety
Chemical Facility Integration Benefits:
  • Digital audit trails for regulatory scrutiny and compliance documentation
  • Connected safety actions linking AI detection with immediate safety workflows
  • Custom detection rules adapted to your chemical plant's PPE requirements and hazard zones.
  • Chemical inventory monitoring for proper toxic and corrosive substance handling.
Multi-Site Chemical Operations:
  • Chemical plant layout optimization for safer processing zone configurations
  • Supply chain safety through improved chemical handling and transfer protocols.
  • Predictive maintenance supported by safety-driven equipment monitoring data.
  • Cross-facility compliance standardization across multiple chemical processing sites.

Top Challenges faced in Warehousing and Logistics Operations

Costly Downtime & Penalties

Accidents and compliance gaps drain productivity and budgets.

Hidden Hazards Everywhere

Forklifts, cluttered aisles, and blind spots often go unnoticed.

Cookie-Cutter Fixes Fail

Generic safety programs miss real, everyday risks.
Advanced Chemical Safety Technology Features

Cutting-Edge AI for Chemical Industry Hazards

Observia combines AI-powered computer vision with chemical-specific IoT sensors to create a connected safety ecosystem that adapts to your chemical processing patterns, continuously improving hazard detection accuracy while reducing false positives in complex chemical environments.

Chemical-Specific Technical Capabilities:

  • AI-driven chemical handling compliance for toxic, corrosive, and flammable substance protocols.
  • Predictive analytics for equipment failure prevention in chemical processing areas.
  • Chemical transfer zone protection through safer loading, unloading, and transport practices.
  • Process safety audits powered by continuous chemical facility monitoring data
  • Confined space monitoring to prevent unauthorized tank and vessel entry violations.
  • Chief AI Assistant for Chemical Operations Analyzes chemical safety trends, identifies SIF root causes, and recommends OSHA-aligned corrective actions

Proven Results for Chemical Safety Excellence.

Our AI-powered monitoring system delivers measurable improvements for chemical processing operations:
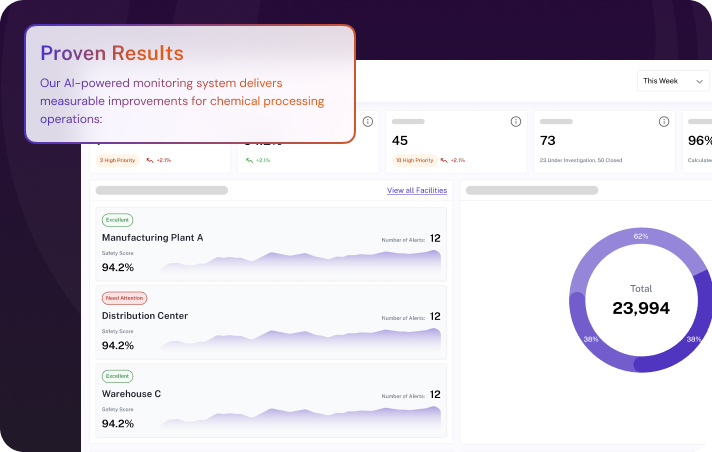
  • Significant reduction in chemical exposure incidents and SIF events
  • Dramatic improvement in PPE compliance rates for face shields, respirators, and chemical-resistant equipment.
  • Higher regulatory compliance audit scores across chemical facilities
  • Reduced insurance claims and liability costs from chemical-related incidents
  • Faster emergency response through real-time chemical hazard detection and alerts
  • Enhanced fire and explosion prevention through continuous ignition risk monitoring

Get in touch with Observia’s Chemical Plant Safetytechnology experts today.

Ready to Transform Your Chemical Plant Safety with Observia.ai?